7. 3D work#
Everything so far has cut 2D geometry to a depth. 3D Profile is different: it follows a surface, taking its shape from an imported STL mesh or a greyscale depth map image, and sweeping a round-nosed cutter back and forth across it until the wood matches the model.
This is how you carve a relief — a sign with a raised crest, a topographic map, a face, anything modelled elsewhere.
Importing an STL#
Import File in the toolbar takes .stl in both binary and ASCII form. Drag-and-drop
onto the canvas works too.
What appears on the canvas is a rectangle, not a mesh — the model's XY footprint at its true size, placed in the middle of the stock. The mesh itself rides along with that rectangle; the rectangle is the handle you use to place and size the carve.
Switch to the 3D View to see the actual model.
Placing and sizing it#
Move and scale the rectangle like any other object (chapter 2). Two things about how that maps onto the carve:
The top of the model becomes the top of the stock. The mesh's highest point is placed at Z 0 and everything else hangs below it, so the whole relief cuts into the board. You don't position it in Z; you decide how deep you'll let it go.
Depth scales with the average of the X and Y scaling. Scale the rectangle uniformly and the relief keeps its proportions — twice as wide is twice as deep. Scale it non-uniformly and the height is scaled by the mean of the two, which will not match either axis, so a stretched model is a distorted one. If you care about the proportions, scale uniformly.
An STL is a surface, and this operation carves it from directly above. Undercuts — anything that overhangs itself — cannot be machined on three axes, and the carve simply takes the highest surface at each point. Model accordingly.
Importing a depth map image#
A depth map is a greyscale picture in which brightness is height: white is the top of the relief, black is the bottom, and every grey is somewhere between. They are the common currency of relief carving — sold as "grayscale reliefs", exported from 3D modelling programs, or generated from an ordinary photo by depth-estimation tools. If you have one, you do not need an STL.
Import File takes PNG, JPEG and WebP. The picture appears on the canvas at its true aspect ratio, and you move, scale and rotate it like any other object. Two differences from an STL:
Width, height and depth are independent. The rectangle sets the carve's width and height exactly; its depth is a setting on the operation (Relief Depth, below), not a consequence of the scaling. Stretching a picture does not distort its depth the way stretching an STL does.
Rotation is followed exactly. A turned picture carves turned, where the canvas shows it.
Prefer PNG. JPEG compression scatters faint specks through a flat background, and while the carve recognises a background and cuts it flat (see below), a clean source is always the better start.
The 3D Profile operation#
Choose 3D Profile, then pick the model from Model: STLs and images are listed separately, under STL and Depth map image. The form has two halves.
Finishing — the pass that makes the surface#
| Field | What it does |
|---|---|
| Tool | Ball nose or taper only. A flat cutter cannot follow a curved surface |
| Stepover (XY) | Spacing between passes, as a percentage of tool diameter |
| Angle | Which way the raster lines run, −90° to +90° |
| Max Depth | How far below the stock top the cut may go |
Stepover is the finish quality control, and it is the expensive one. The cutter is round, so between two adjacent passes it leaves a ridge — a scallop. Halving the stepover halves the scallop height and doubles the number of passes, and 3D finishing passes are long to begin with. A small ball nose at a fine stepover can run for hours.
On a taper, stepover is a percentage of the tip, not of the cutting diameter. A 30% stepover on a 2 mm tip is 0.6 mm — the form spells the millimetres out beside the percentage, which is the number to judge.
Pick the angle to run the passes along the length of the detail rather than across it — a face reads better rastered vertically, a long ridge along its own axis.
Roughing — the pass that saves the finishing cutter#
Optional but almost always worth it. Without it, the finishing tool has to remove everything, taking full-depth cuts with a small round bit — slow, and hard on the cutter.
| Field | What it does |
|---|---|
| Roughing tool | A bigger ball nose or a flat end mill. An end mill takes level ground — the floor round a relief — straight to its final depth, leaving the finish nothing to do there. None gives a single-pass job |
| Roughing stepover | Wider than the finishing stepover — this pass is for volume, not finish |
| Roughing step down | Axial depth per level |
| Roughing angle | Defaults to 90° from the finishing angle, so the finish pass crosses the roughing marks |
| Stock allowance | Material left for the finishing pass — 0.3 mm by default |
The finishing pass is rest-machined: it knows what roughing already removed and only cuts what's left, so it doesn't waste time cutting air over ground that's already clear.
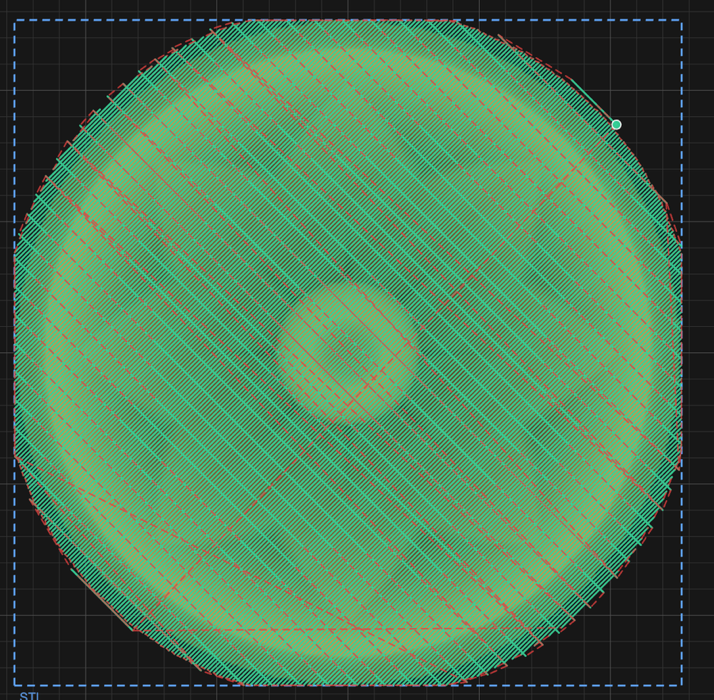
Both passes drawn together. Finishing is set to 45°, so roughing defaults to 135° and the two cross at a right angle — finishing across the roughing grooves cuts a more even chip than following them.
A depth map's height#
Pick an image as the model and two fields appear under it:
| Field | What it does |
|---|---|
| Relief Depth | How far the picture's background lies below its white — the height of the carve |
| Dark is high | Turns the picture over: black becomes the top and the lightest part the bottom |
White sits at the top of the stock — or Model Top Below Stock lower, if you set it — and the background sits Relief Depth below that. The greys in between are spread evenly across the depth.
The background is found, not assumed. A depth map's background is rarely pure black: it may be a dark grey, and a JPEG's black is a dense cluster near 0 with compression specks scattered out to grey 20 or more. Taking black as the bottom would leave a grey background standing proud of the floor cleared round the picture, and would carve every speck as a bump. So the carve finds the background as the cluster of near-identical darks at the bottom of the picture's tones, takes in its specks, and cuts everything at or darker than it flat on the floor. The form shows where it landed — Background: grey 28 and below — so you can check it before generating. A picture with no flat background, only content, uses its darkest tones, ignoring the darkest 0.1 % so a few specks cannot decide it. With Dark is high all of this is mirrored: the background is the light cluster at the top.
Two things to keep in mind:
- A picture has 256 grey levels, so the height comes in up to 256 steps. On a 12 mm relief each step is under 0.05 mm, finer than a ball nose's scallops — but a picture that uses only a narrow band of greys has fewer steps than that across the same depth.
- Max Depth still caps the cut. If Model Top Below Stock plus Relief Depth goes deeper than Max Depth, the lowest part of the picture is cut flat at Max Depth, and the form says so under Relief Depth.
A depth map is finished with the Raster strategy only; Waterline is not offered for an image.
Clearing round it#
With Boundary left at Model box, the carve covers the picture's own rectangle and nothing else. Draw a closed shape round the picture and pick it as the Boundary instead, and everything inside that shape which the picture does not cover is cleared down to the background level — the picture stands as a relief in a recessed field, with the tool's edge kept inside your shape. Pick Stock to clear to the board's own edges.
Around a boundary the finish does not visit ground the roughing has already finished: each raster row turns round where the relief's work ends, and one lap of the boundary at the end cleans the edge.
Example — a depth-map plaque#
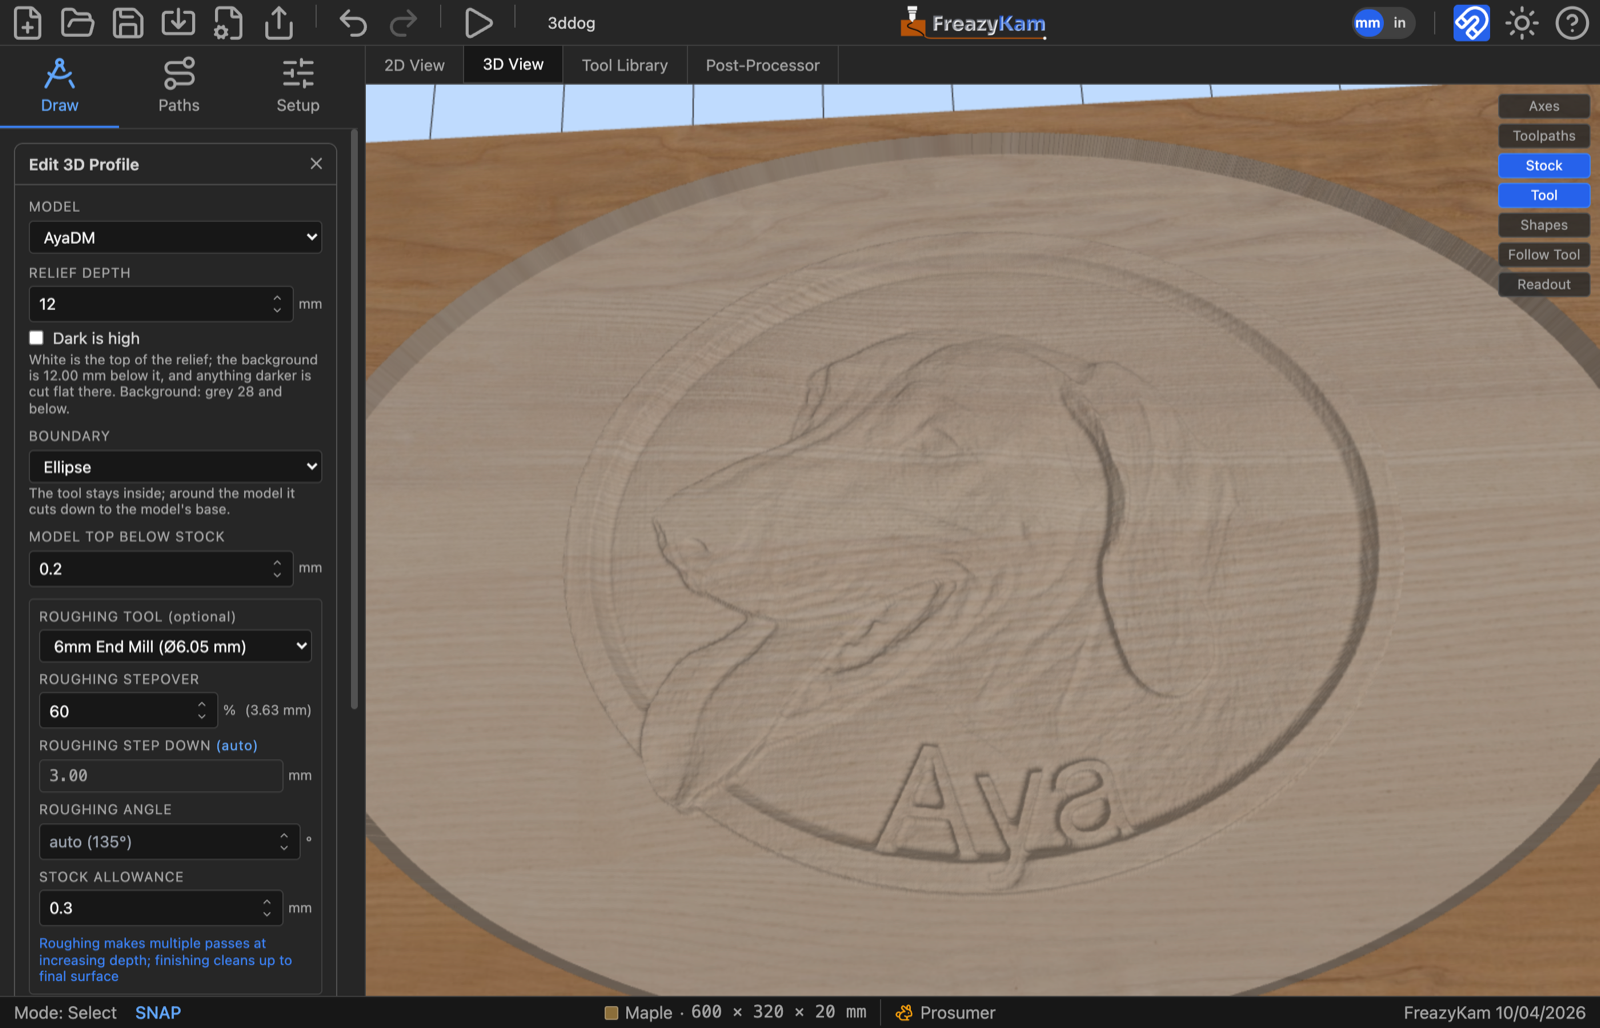
A greyscale depth map of a dog plaque, carved into maple. The picture is the model, an ellipse drawn round it is the boundary, so the field around the plaque is cleared down to its background. Settings: Relief Depth 12 mm with the background found at grey 28, Model Top Below Stock 0.2 mm so the plaque's rim is skimmed rather than left as raw stock, a 6 mm end mill roughing at 60 % stepover, and a 1/8" ball nose finishing at 20 % (0.64 mm) on a 45° raster.
The order of work for a job like this:
- Import the picture and size it on the stock. Scale it uniformly unless you mean to change its proportions.
- Draw the boundary — here an ellipse — enclosing the whole picture.
- 3D Profile: pick the picture as the Model and the ellipse as the Boundary, set Relief Depth, and check the Background readout under it.
- Add an end mill as the roughing tool. On a plaque most of the volume is the open field, which the end mill clears to its finished depth outright.
- Generate, then simulate in the 3D view before trusting it.
Checking it#
The 3D View is not optional on this kind of job. A relief has no outline to sanity-check on the 2D canvas; the toolpath is thousands of near-identical passes and reading it tells you nothing.
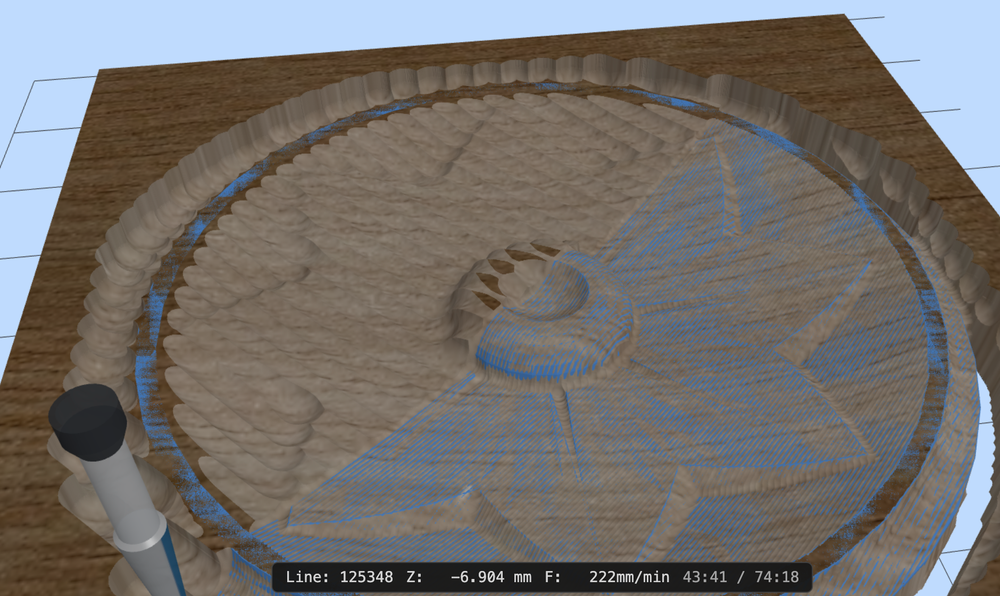
Part way through a relief. The ridges around the rim are roughing scallops the finishing pass hasn't reached yet — and the clock says 43:41 of 74:18.
Simulate, then look at the carved surface. What you are checking for:
- Scalloping you can see in the render will be there in the wood.
- Flat spots where the tool was too big to reach into a hollow. A ball nose cannot cut a valley tighter than its own radius, and the simulation shows exactly that.
- A relief that bottoms out, meaning Max Depth clipped the model rather than the model fitting the board.
And check the estimated run time in the export review before committing. 3D finishing is where a job quietly turns into an overnight one.
Next#
- 8. Parametric parts — gears, clocks, track and cutting boards
- 10. Simulating and exporting — the review before you cut